
TTM Technologies Supports Sensitive Manufacturing with an ISO 7 Cleanroom Expansion
ProPart Modular is excited to continue collaborating with TTM technologies, a global innovator in mission-critical technologies, microelectronic assemblies, and more. TTM Technologies has been a valued customer of ProPart Modular for more than 25 years. As part of their manufacturing expansion, TTM required an additional 28′ × 44′ ISO 7 cleanroom. This cleanroom supports the production […]

Concept Storage Solutions Goes Vertical to Create New Office Space
ProPart Modular’s System 40™ Two Storey was the perfect solution for Concept Storage Solutions. This created two separated areas, all while utilizing floor space. A custom two storey 20’ x 30’ unit was designed and installed with upper floor stair access and windows. By going vertical, Concept Storage Solutions was able to continue using the […]
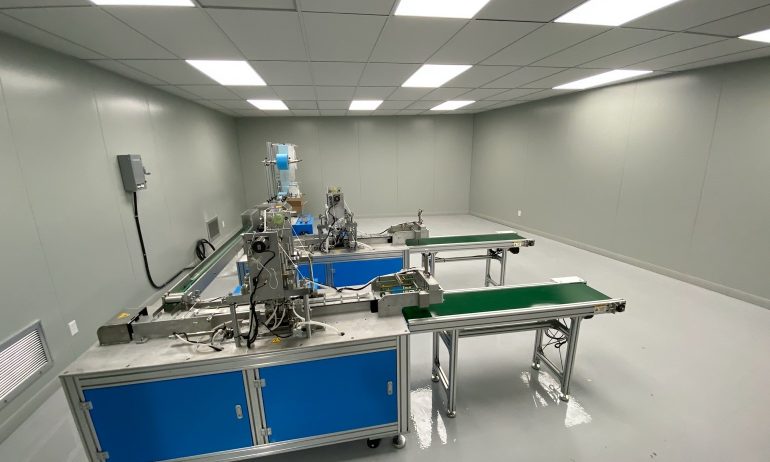
Trico’s Canadian PPE Solution
When Trico Packaging and Print Solutions Inc. needed a new controlled environment to manufacture and test face masks, they turned to ProPart Modular to get the job done quickly and efficiently. With Canada’s frontline healthcare workers in need of supplies, Trico began to transition, pivoting away from its traditional print business to make ASTM F2100 […]
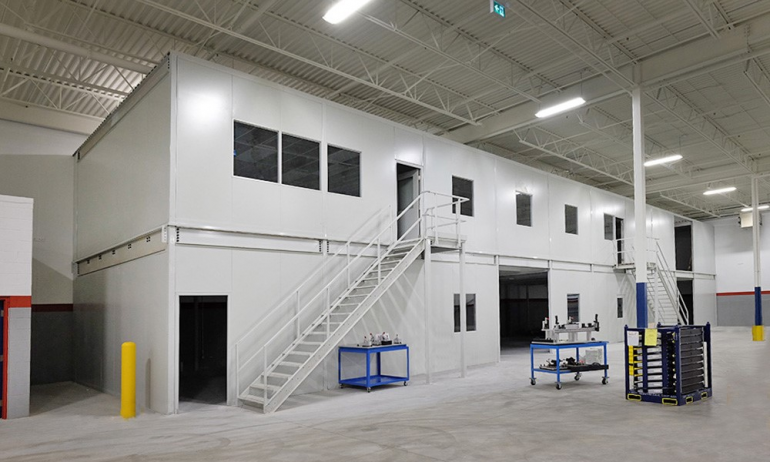
Multimatics’ System 40™ Quality Assurance Lab
Multimatics new quality assurance lab is a testament to the flexibility and re-purposing of ProPart’s System 40™ mezzanine and in plant office components. Multimatics new structure is composed entirely of standard System 40™ parts from a previous installation…
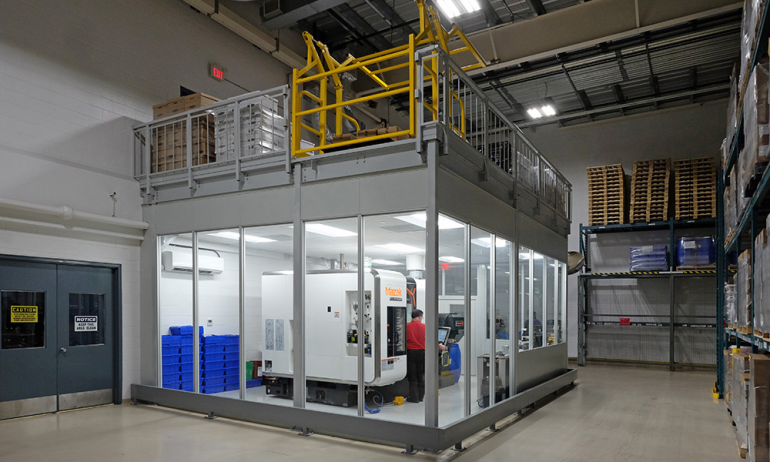
Catalent System 40™ CNC Enclosure
Catalent (formerly Accucaps) approached ProPart to construct a CNC enclosure for their busy manufacturing facility located in Strathroy, Ontario…
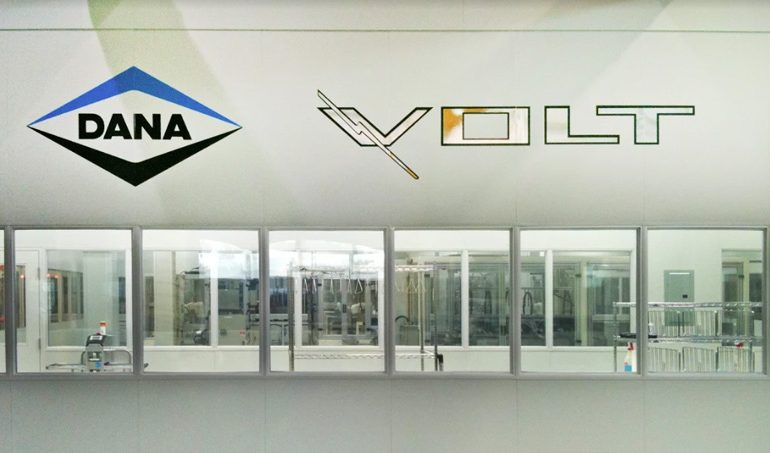
Dana Canada Corporation
Dana Canada, a corporation based out of Cambridge, ON, needed a supplier with a longstanding expertise in the manufacture and installation of clean rooms to install a 3,000 square foot clean room in an existing facility. As a specialist in providing modular Clean Room structures, ProPart Modular is easily able to meet ISO Class 7, which requires […]
Konecranes Canada…Their Problem, Our Solution
Konecranes Canada approached ProPart Modular among other providers, for a quote to construct 3 new In Plant Offices and a storage Mezzanine for their new state-of-the-art head office in Burlington, Ontario. One of their primary concerns was sound reduction for the office, as they would be situated in a high traffic area. Not only would […]
Cyclone’s Quality Control Room Wall
Case History Example: Cyclone Manufacturing Toronto, Ontario Canada Problem: Cyclone Manufacturing needed to separate a 5,400 square foot quality control section from the main production area. Solution: Repeat customer Cyclone Manufacturing turned to ProPart Modular for yet another modular space solution. Combining a mezzanine storage area above the quality control department made it possible to […]
Technophar Clean Room
Case History Example: Technophar Equipment & Services Ltd. Windsor, Ontario Problem: Technophar Equipment and Services Ltd., a manufacturing company primarily servicing the pharmaceutical industry, needed a large Clean Room facility to showcase their custom manufactured packaging line equipment. Solution: After doing the research, they opted for a ProPart Modular modular space solution, largely because of ProPart’s proven […]
Cocomira’s System 40™ Divider Wall
Case History Example: Cocomira Toronto, Ontario Canada Problem: Preparing gourmet toffee in the food industry is not for everyone. Because it generates so much heat many won’t even attempt it. To manage the heat in their facility, Anna Janes, founder of Cocomira, needed to section off the kitchen from the production area. Solution: Working closely […]